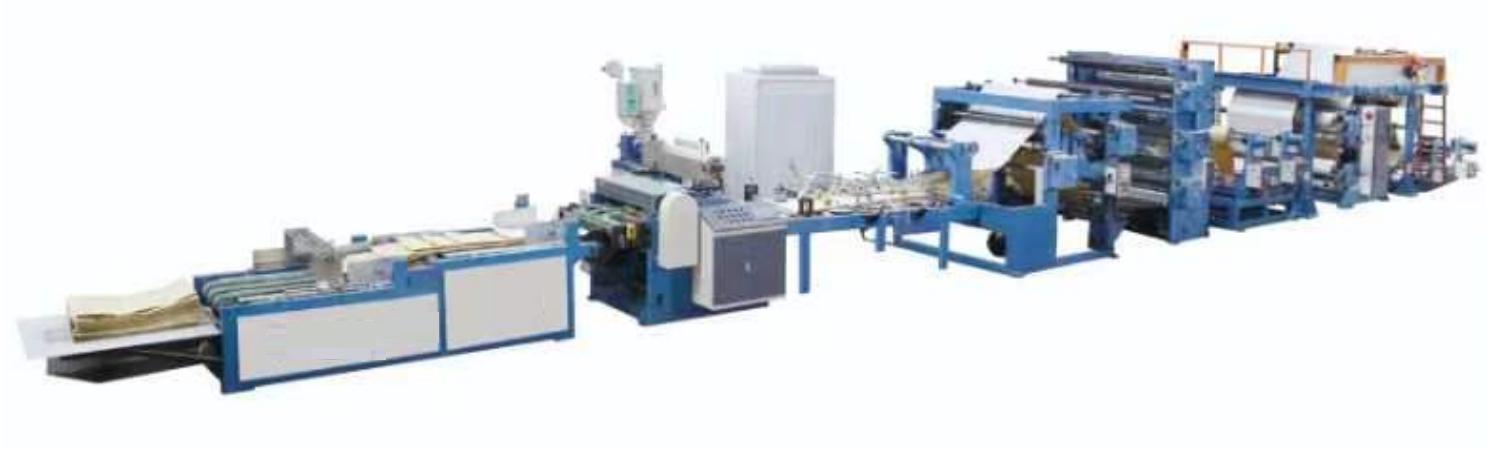
Common problems and troubleshooting methods for PP flat yarn drawing machines
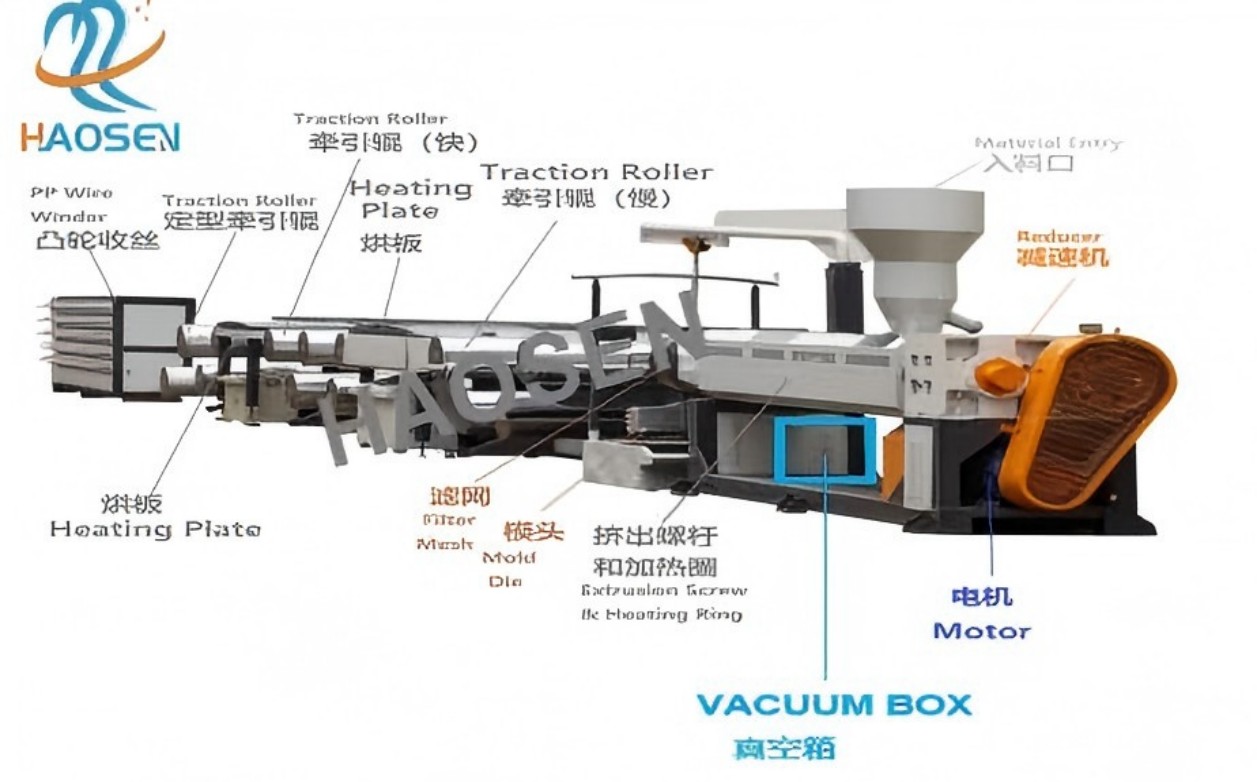
一、挤出系统故障 Extrusion System Faults
|
故障现象 Fault Phenomenon
|
原因 Causes
|
排除方法 Solutions
|
|
不出料、出料量不足
No material output / Insufficient output
|
料斗堵塞、进料段温度过高、滤网堵塞、螺杆卡异物、原料受潮结块
Hopper blockage, over-high feeding temperature, screen clogging, foreign matters on screw, damp and caked materials
|
清理料斗及螺杆异物、降低进料段温度、按时换网、原料烘干除结块
Clean foreign matters, reduce feeding temperature, replace screen regularly, dry raw materials
|
|
挤出电流波动不稳
Unstable extrusion current
|
原料含水含杂、温控不均、螺杆磨损、变频器转速不稳
Moisture/impurities in materials, uneven temperature, worn screw, unstable inverter speed
|
原料烘干除杂、检修温控、更换磨损螺杆、校准变频器
Dry and purify materials, repair temperature system, replace screw, calibrate inverter
|
|
模头出料不均、膜厚偏差大
Uneven die output & film thickness deviation
|
模头温度不均、模唇间隙不均、滤网局部堵塞、冷却水不稳
Uneven die temperature, inconsistent lip gap, partial screen blockage, unstable cooling water
|
检修模头加热、微调模唇间隙、更换滤网、稳定水温和牵引速度
Check die heater, adjust lip gap, replace screen, stabilize water and traction speed
|
|
平膜气泡、气孔、鱼眼
Bubbles, pores, fish eyes on film
|
原料水分超标、温度过高降解、杂质多、模头碳化积料
Excessive moisture, thermal degradation, many impurities, carbonized residue in die
|
彻底烘干原料、适当降温、清理模头碳化料、低速排气
Fully dry materials, lower temperature, clean die carbonization, run at low speed for exhaust
|
|
模唇挂料、产生塑珠
Die lip hanging material & plastic beads
|
烘干异常、模温偏高、熔体流动性差
Abnormal drying, excessive die temperature, poor melt fluidity
|
调整烘干工艺、降低模温、清理模口积料抛光模唇
Adjust drying process, reduce die temperature, clean and polish die lip
|
二、平膜成型故障 Flat Film Forming Faults
|
故障现象 Fault Phenomenon
|
原因 Causes
|
排除方法 Solutions
|
|
膜面直条纹、划痕
Stripes and scratches on film
|
模唇卡杂质、模唇磨损、冷却辊脏污
Lip dirt, worn die lip, dirty cooling roller
|
清理模唇、修复磨损部位、清洁冷却辊
Clean lip, repair worn parts, clean cooling roller
|
|
薄膜起皱、两边紧中间松
Film wrinkling & uneven tension
|
模头两端温度低、冷却水不均、牵引张力失衡
Low temperature on both sides, uneven cooling water, unbalanced tension
|
升高模头两侧温度、平衡水路、校正牵引辊平行度
Raise die side temperature, balance water flow, calibrate roller parallelism
|
三、牵伸剖丝核心故障 Drawing & Slitting Faults
|
故障现象 Fault Phenomenon
|
原因 Causes
|
排除方法 Solutions
|
|
扁丝频繁断丝
Frequent wire breakage
|
牵伸比过大、烘箱温度异常、原料韧性差、辊筒打滑
Excessive drawing ratio, abnormal oven temperature, poor material toughness, roller slipping
|
降低牵伸比、校准烘箱温度、更换原料、清洁辊筒增摩擦
Reduce drawing ratio, calibrate oven temperature, change materials, clean rollers
|
|
竹节丝、粗细不均
Bamboo-joint wire & uneven thickness
|
水温高、速度波动、原料未烘干、温度不稳
High water temperature, speed fluctuation, undried materials, unstable heat
|
降温增水流量、稳定转速、彻底烘干原料、恒温生产
Lower water temperature, stabilize speed, fully dry materials, constant temperature
|
|
剖丝跳刀、切口不齐
Slitting jumping & uneven cutting
|
刀片钝、角度不准、模温高、膜张力不稳
Dull blade, wrong angle, high die temperature, unstable film tension
|
更换新刀片、校正角度、降低模温、稳定膜张力
Replace blade, correct angle, reduce die temperature, stabilize film tension
|
四、收卷、机械与电气故障 Winding, Mechanical & Electrical Faults
|
故障现象 Fault Phenomenon
|
原因 Causes
|
排除方法 Solutions
|
|
收卷松紧不一、堆垛
Uneven winding & stacking
|
张力控制器失灵、收卷辊磨损、传感器故障
Failed tension controller, worn roller, faulty sensor
|
校准张力、更换辊筒、检修传感器、匹配速度
Calibrate tension, replace roller, repair sensor, match speed
|
|
设备震动大、异响
Severe vibration & abnormal noise
|
轴承缺油损坏、螺丝松动、齿轮不良、机座不稳
Damaged bearings, loose screws, poor gear meshing, unstable base
|
补高温润滑脂、紧固螺丝、检修齿轮、加固机座
Add high-temperature grease, fasten screws, repair gear, fix base
|
|
无法启动、温控失灵
Startup failure & temperature control failure
|
缺相、探头损坏、急停未复位、线路松动
Phase loss, broken probe, unreset emergency stop, loose wiring
|
检修电源、更换探头、复位急停、紧固线路
Check power supply, replace probe, reset stop button, fasten wires
|
五、日常维保标准 Daily Maintenance Standards
1. 原料管控 Raw Material Control
新料、再生料必须烘干除杂,严禁含水原料上机。
Virgin and recycled materials must be dried and purified. Wet materials are prohibited.
2. 滤网更换周期 Screen Replacement Cycle
全新原料 72 小时换网,再生料 40 小时以内强制换网。
Screen change every 72 hours for virgin material, within 40 hours for recycled material.
3. 温度管控 Temperature Control
严控挤出、模头、烘箱温度,杜绝物料碳化。
Strictly control extrusion, die and oven temperature to prevent carbonization.
4. 润滑保养 Lubrication
轴承、减速机定期补油,高温部位使用耐高温润滑脂。
Regular lubrication for bearings and reducers; use high-temperature resistant grease.
5. 每日清洁 Daily Cleaning
停机清理模唇、冷却辊、牵引辊积料,防止划伤薄膜扁丝。
Clean die lip and rollers after shutdown to avoid scratches.
六、紧急停机条件 Emergency Shutdown Rules
1. 大面积连续断丝无法恢复 Continuous large-area wire breakage
2. 模头严重挂料、碳化冒烟 Severe die hanging material and smoking
3. 设备剧烈震动、异响、皮带打滑冒烟 Severe vibration, abnormal noise and belt slipping
4. 电气报警、温控失效、电机过热 Electric alarm, temperature failure and motor overheating